


recommend
Send Us A Message
Ferroalloys in Steelmaking: How Recovery Rates Affect Alloy Additions
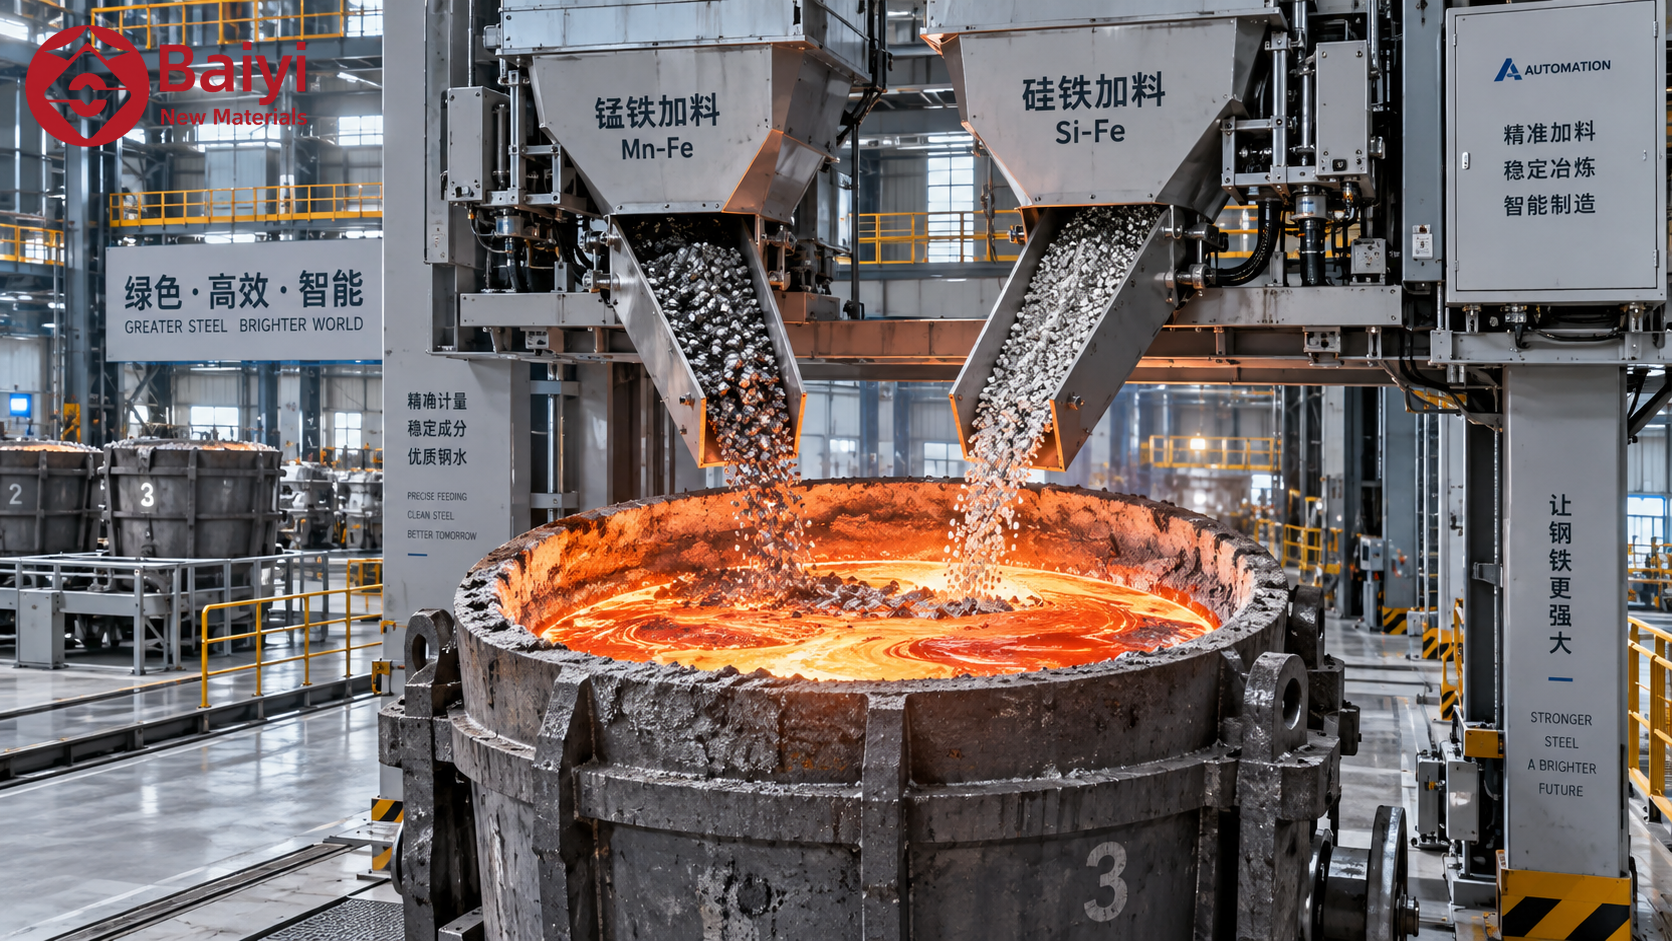
Ferroalloys should be dosed according to the amount of alloying element expected to remain in the steel, rather than the amount charged. A certificate showing manganese or silicon content establishes the input composition; it does not establish how much the bath will retain. Using an unsuitable recovery assumption can produce an off-specification heat even when the weighing and alloy analysis are correct.
The useful recovery value is specific to an element, a process stage, and a sampling endpoint. It must account for the conditions under which the addition dissolves, reacts, and remains in the steel.
Define recovery before calculating an addition
Elemental recovery is the net increase in the mass of an element in the steel, attributable to an addition, divided by the mass of that element charged. Expressed as a percentage:
Recovery (%) = element mass retained from the addition ÷ element mass charged × 100
This is different from the percentage of alloy that physically dissolves. An addition may dissolve but then lose part of its manganese or silicon to oxidation. Conversely, a sample taken before dissolution and mixing are complete can indicate a low apparent recovery even though more of the element will subsequently enter the sampled bath.
For alloys containing several useful elements, calculate recovery separately for each one. Silicomanganese, for example, supplies both manganese and silicon, but those elements need not have the same recovery.
Calculate the elemental shortfall, then allow for losses
For a preliminary calculation where the addition is small relative to the steel mass, use:
Alloy addition mass ≈ M × (wtarget − winitial) ÷ (x × R)
- M: liquid steel mass before the addition.
- wtarget and winitial: target and initial mass fractions of the element in steel.
- x: mass fraction of that element in the ferroalloy.
- R: expected elemental recovery, expressed as a decimal.
Keep all composition inputs on the same basis. Convert percentages to mass fractions before using this equation, and use consistent mass units. The calculation shows why a higher alloy assay does not automatically mean a lower required charge: its advantage can be offset by lower recovery.
This approximation treats steel mass as effectively constant. When additions materially change bath mass, use a full mass balance that includes the final steel mass and the retained contributions of all additions. Where several materials supply the same element, include every source rather than assigning the entire chemistry increase to one ferroalloy.
Check the other elements introduced by the calculated dose. A manganese addition may also introduce carbon, silicon, phosphorus, or sulfur. Meeting the manganese target does not establish that the resulting steel meets the complete grade specification.
Why ferroalloy recovery changes between heats
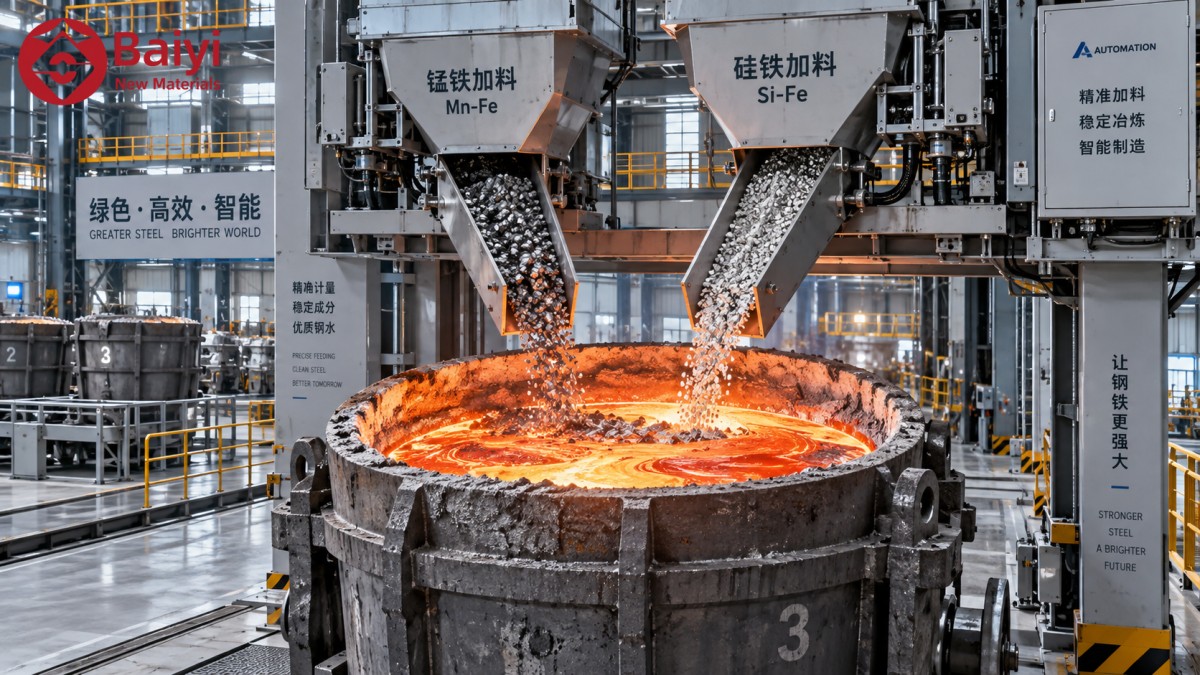
Oxygen activity and slag oxidation state directly affect losses. Dissolved oxygen and oxidizing slag constituents can consume alloying elements. Ferrosilicon added for deoxidation therefore serves a different purpose from a silicon trim added after oxygen has been reduced. Treating both additions as having one recovery factor can distort the charge calculation.
Slag basicity alone is insufficient to predict recovery. Slag composition, oxide activities, slag quantity, and contact with the metal all influence reactions. Oxidizing slag carried over from an earlier stage can change the result even when the alloy grade and charge weight remain constant.
Temperature, particle size, and mixing affect dissolution and distribution. Large pieces may require more time to dissolve; excessive fines can be lost through dust generation or oxidize readily during handling and charging. An appropriate size range depends on the charging route, bath conditions, and available mixing time.
Addition timing changes both exposure to oxidation and the time available for dissolution. A late addition may encounter more favorable chemical conditions but leave too little time for complete mixing before sampling or casting. Moving additions later is therefore not a universal route to higher recovery.
Build a recovery basis that supports reliable decisions
Use operating records from comparable heats to establish recovery assumptions. Group results by alloy grade, addition stage, deoxidation practice, slag conditions, temperature range, and mixing practice. A single average across different routes can conceal the variation that causes missed chemistry targets.
For each calculation, record the steel mass, initial analysis, weighed additions, alloy batch analysis, and final sample timing. Account for intervening additions and other element sources or losses. Apparent recovery above complete retention usually signals an incomplete accounting boundary, sampling differences, or measurement uncertainty; it should not become a routine dosing assumption.
Supplier comparisons should include chemical analysis, relevant impurity limits, particle size distribution, fines, and batch consistency. A product specification can define the supplied material, but a recovery claim requires stated operating conditions and a measurement method.
Compare cost per unit of retained element using alloy price per unit mass ÷ (element fraction × recovery). Then consider recovery variability alongside the average: inconsistent performance can increase corrective additions and make narrow chemistry limits harder to control.
Before changing a dosing rule, establish which part of the calculation has changed: the elemental shortfall, the alloy composition, or the recovery under the actual process conditions. Each requires a different correction.